In this guide 8 sections
Select by removal duty and required finish
Metal-bond and resin-bond squaring wheels are selected for the work each station must do. Review the material, incoming allowance, required finish, machine and operating mode together. A stock-removal stage and a fine-finishing stage can need different wheel specifications even when their diameters and mounting dimensions match.
Establish the geometry, then refine the surface
01Size and squareness
A stock-removal station establishes the edge position and leaves a controlled allowance.
02Fine edge finish
A later station refines the surface it receives. It cannot reliably hide a deep earlier defect.
Compare their roles on the line
| Selection question | Metal-bond options | Resin-bond options |
|---|---|---|
| What task is being reviewed? | Size control, stock removal or a defined intermediate stage | Fine grinding and edge refinement on compatible materials |
| What construction is available? | Segmented or continuous designs, depending on the series | Continuous or slotted options in the resin squaring range |
| What else affects the result? | Grit, bond formulation, contact and machine conditions | Grit, bond formulation, incoming surface and finishing allowance |
| What needs confirming? | Exact material, wheel dimensions and approved mode | Exact material, wheel dimensions and approved mode |
Compare the options Tap to expand
What task is being reviewed?
- Metal-bond options
- Size control, stock removal or a defined intermediate stage
- Resin-bond options
- Fine grinding and edge refinement on compatible materials
What construction is available?
- Metal-bond options
- Segmented or continuous designs, depending on the series
- Resin-bond options
- Continuous or slotted options in the resin squaring range
What else affects the result?
- Metal-bond options
- Grit, bond formulation, contact and machine conditions
- Resin-bond options
- Grit, bond formulation, incoming surface and finishing allowance
What needs confirming?
- Metal-bond options
- Exact material, wheel dimensions and approved mode
- Resin-bond options
- Exact material, wheel dimensions and approved mode
These are application roles to discuss with the supplier. The required removal, line condition and complete wheel specification determine whether a particular configuration fits a station.
Compare three product families
The segmented ceramic series is described for wet edge processing. The continuous metal-bond series and resin-bond range offer different constructions and dimensions. Check the operating mode for the exact item, rather than transferring the rating from another wheel in the group.
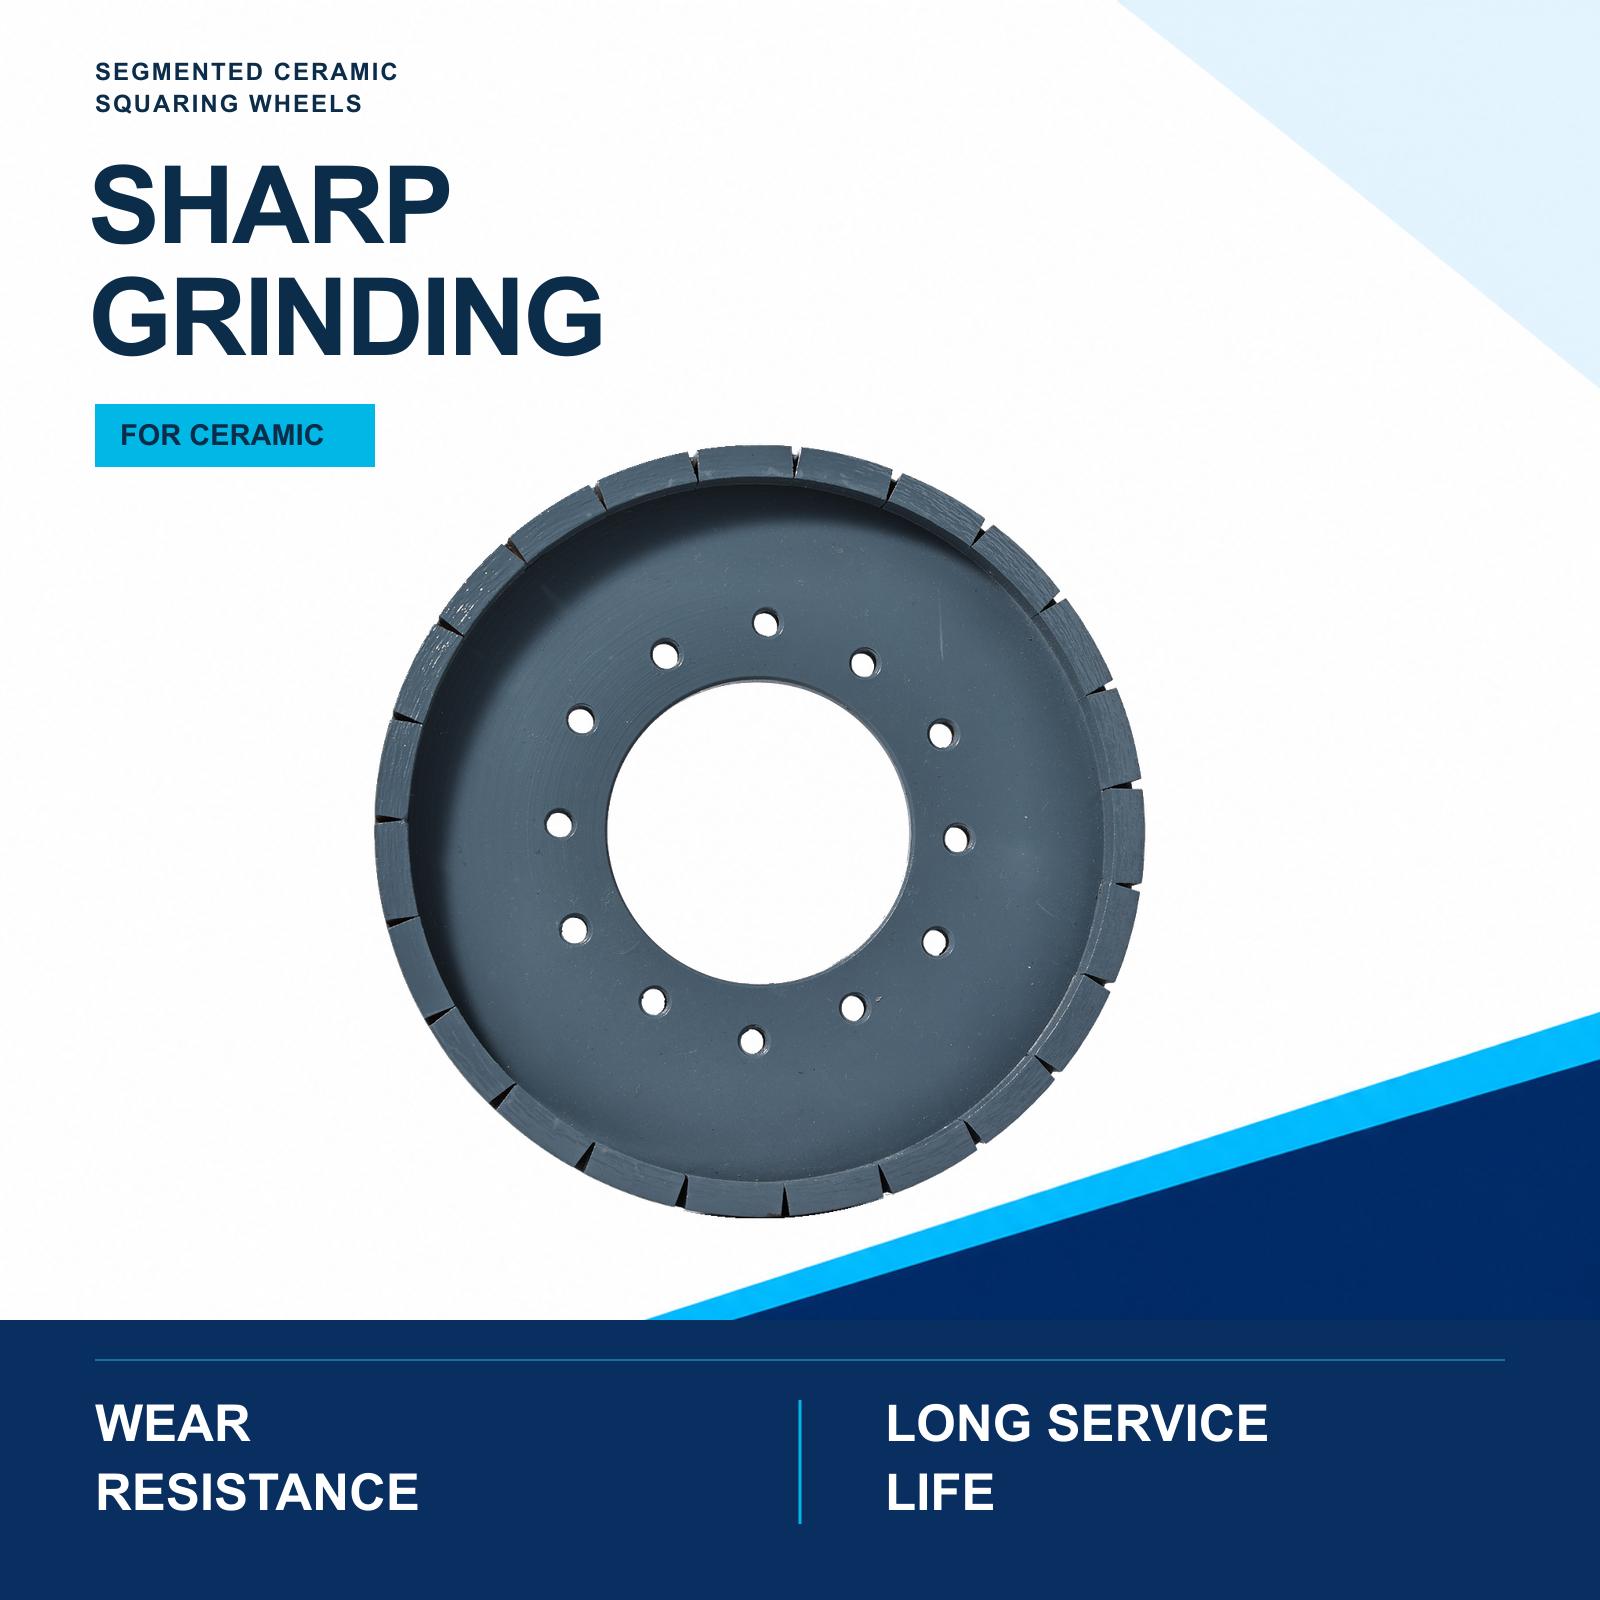
Segmented Ceramic Squaring Wheels
This segmented series is for wet ceramic edge processing. Match the grinding head, working section, bore and fixing holes; choose the grit and process stage together with the incoming edge condition.
View specifications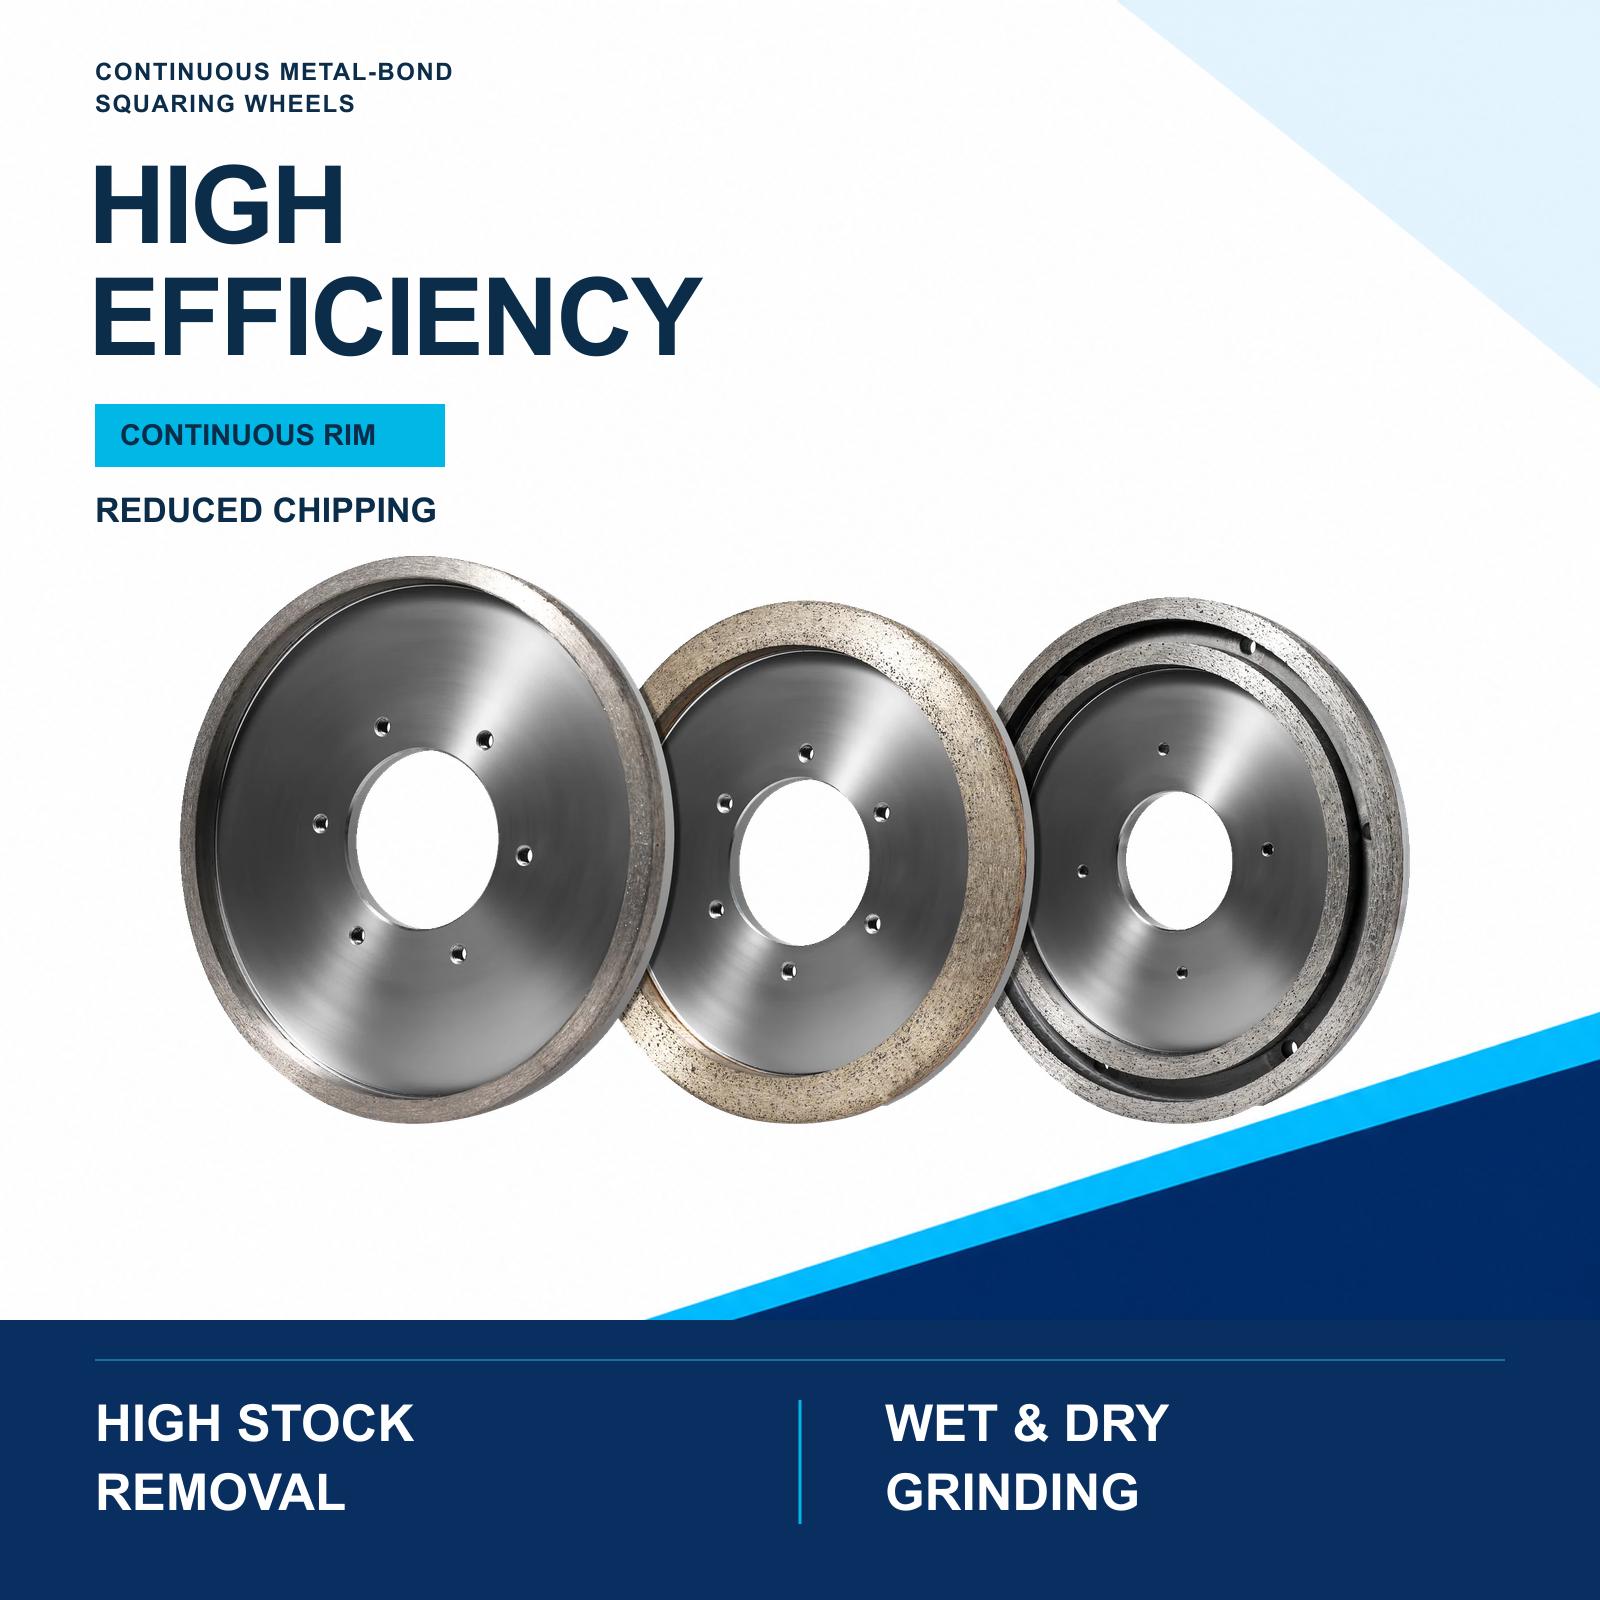
Continuous Metal-Bond Squaring Wheels
Consider this metal-bond series for dry or wet ceramic and sintered-stone edge grinding. Compare the stock-removal task with the later finishing requirement before choosing the working section and grit.
View specifications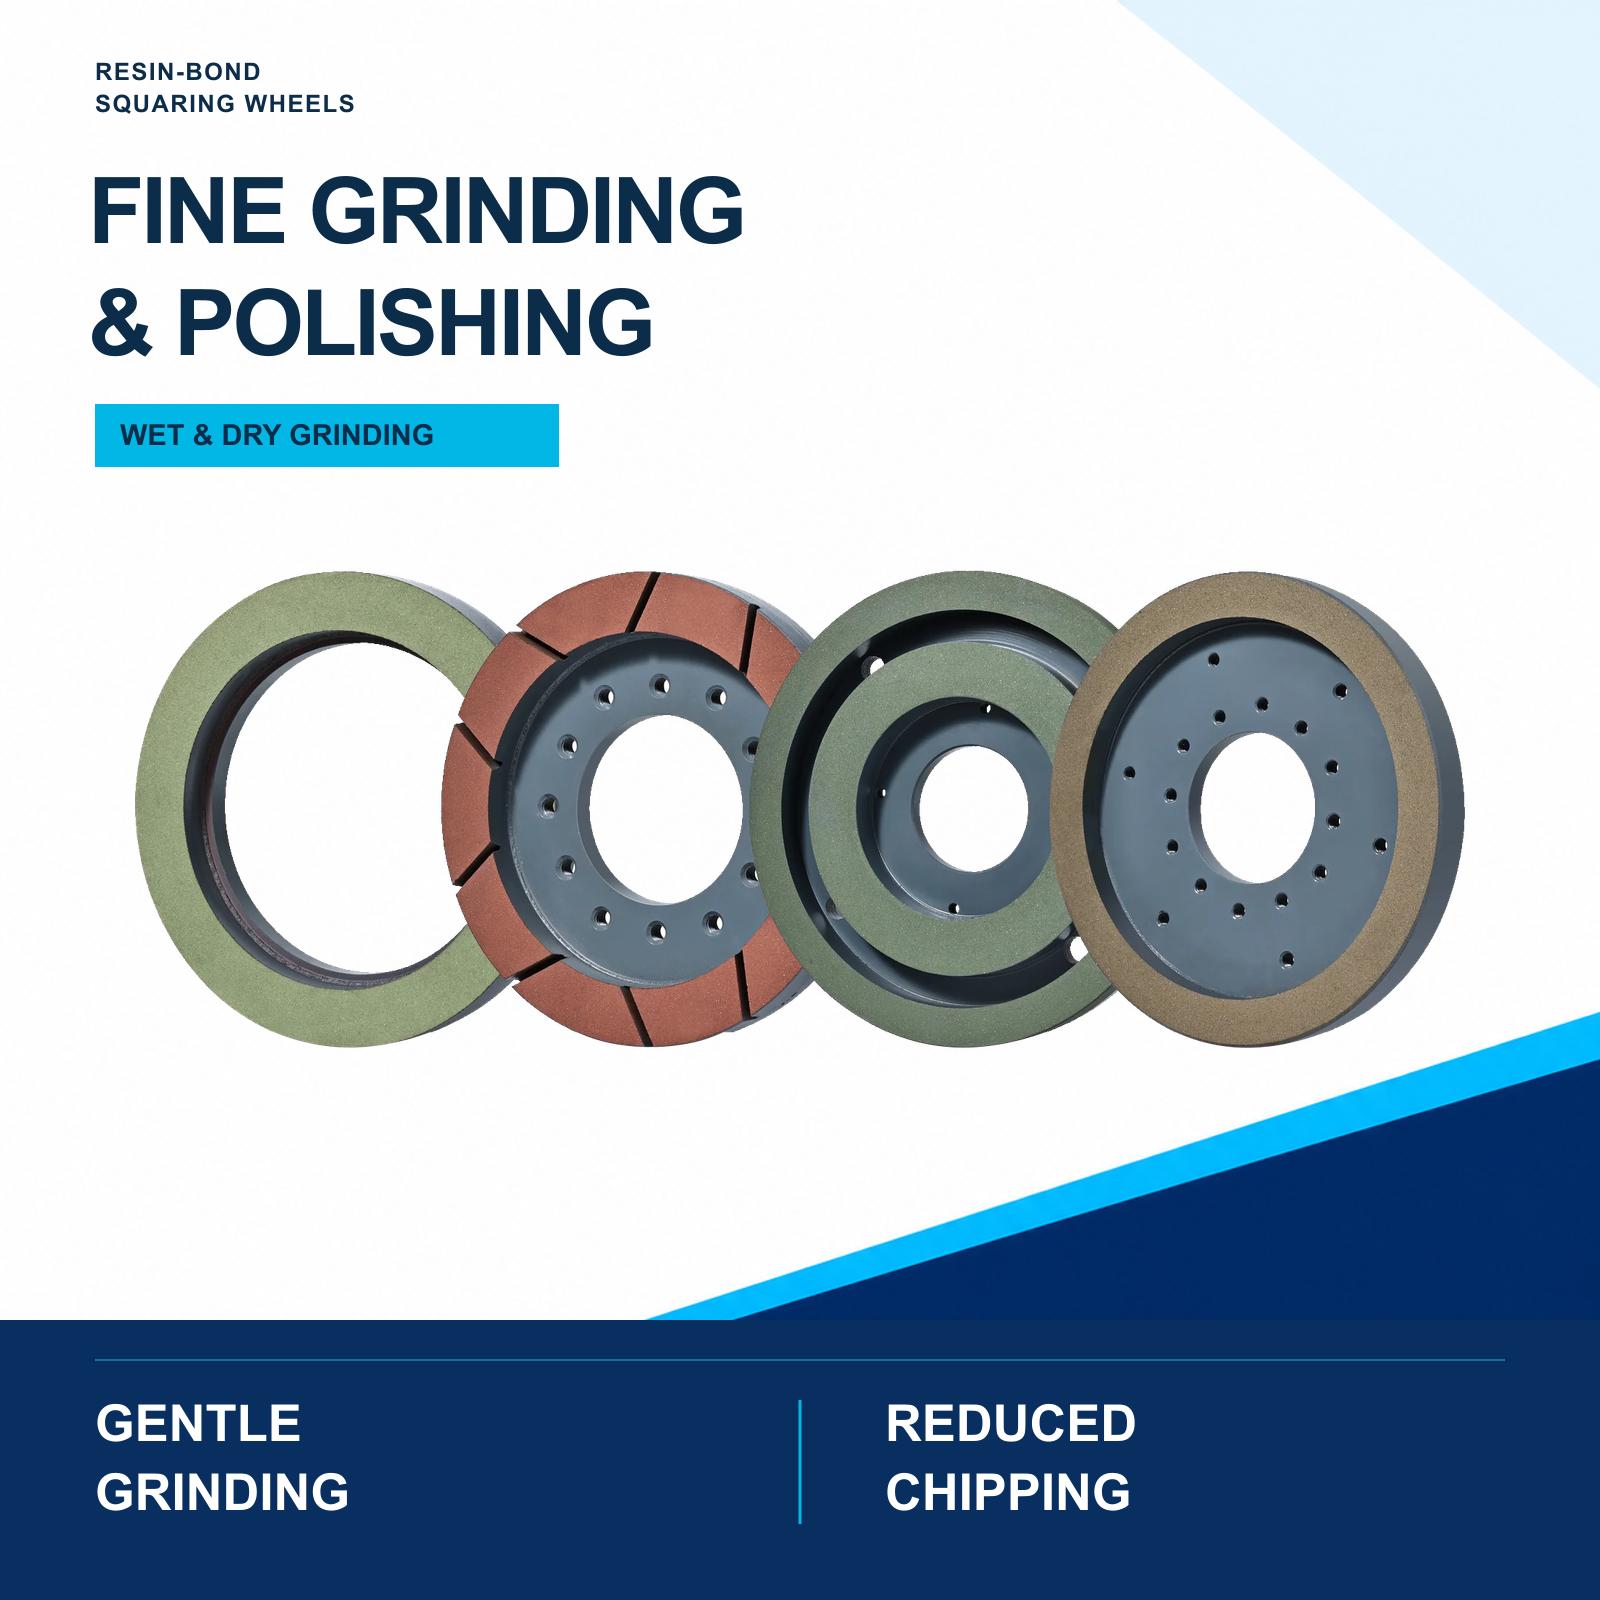
Resin-Bond Squaring Wheels
Choose the resin-bond configuration for the fine-grinding or trimming stage and its dry or wet method. Include the preceding wheel, incoming edge condition and required finish when comparing grit options.
View specificationsFor each candidate, compare diameter, bore, segment dimensions, grit and structure. Ask how the proposed wheel fits between the preceding and following stations. A direct swap based on diameter alone can change contact, removal and the surface delivered downstream.
Diagnose the sequence before changing the final wheel
Follow one edge through the stations
- 01
Incoming edge
Record size variation, cut marks and chips before the first wheel.
- 02
After each station
Record the wheel identity, grit, removal allowance and edge condition.
- 03
First point of failure
Find where the defect appears or stops improving before changing the final wheel.
- 04
Finished tile
Check size, squareness and the agreed visual finish together.
Inspect where the defect begins. Record edge condition, wheel identity and removal allowance at the relevant stages. If a deep chip is present before the resin stage, determine whether the preceding operation is producing acceptable input before asking the fine wheel to remove it.
Norton’s grinding selection guidance treats finish, contact, coolant and power as connected factors. Include those conditions when comparing wheel families.
Selection example: changing an intermediate station
Suppose an intermediate metal-bond wheel is being considered for replacement by a resin-bond option. First record the incoming marks and the amount that the station must remove. Check whether the proposed wheel can perform that duty within the machine’s approved conditions and leave the right input for the next stage.
Compare the edge after that station and at the end of the line. Record size, squareness, surface and wheel condition. Do not approve a change from the appearance of the intermediate edge alone.
Confirm mounting and operating conditions
Check the approved bore, mounting arrangement, speed and wet/dry process. Inspect spindle condition and alignment when installing a different wheel. Keep the line’s cooling or dust-control provisions appropriate to the tool and material.
A repeated scratch, one-sided wear or size drift may involve the machine or setup. Record those symptoms alongside the wheel specification so the supplier can review the full process.
What to include in the quotation request
Send the tile material and thickness, machine model, station layout, current wheel sequence and the defect or improvement being targeted. Include wheel diameter, bore, cutting-section dimensions and grit designations. If cost is the priority, compare accepted finished tiles and the work needed to obtain them, alongside the purchase price.
FAQ
Is metal bond better than resin bond?
No. They commonly serve different process stages. Metal-bond wheels are often evaluated for removal and geometry control, while resin-bond wheels are often evaluated for refinement. The right choice depends on material, machine, method and accepted edge.
Can the same grit be substituted between metal and resin wheels?
Not automatically. The bond and wheel construction change cutting behavior. Treat the supplier’s grit designation as one field in a complete configuration and validate the substitution with a controlled trial.
How do I know which station causes chipping?
Inspect and photograph the edge before and after each station during a controlled setup. Record when the defect first appears. Also inspect upstream cutting because grinding may reveal or enlarge existing damage.
Should I buy one wheel or a complete sequence?
That depends on the problem. Even when buying one wheel, provide the complete existing sequence. The supplier needs to understand incoming and downstream stages to recommend the role of the requested wheel.